Comparing Capped Vias and Other Via Technologies for Modern PCB Designs
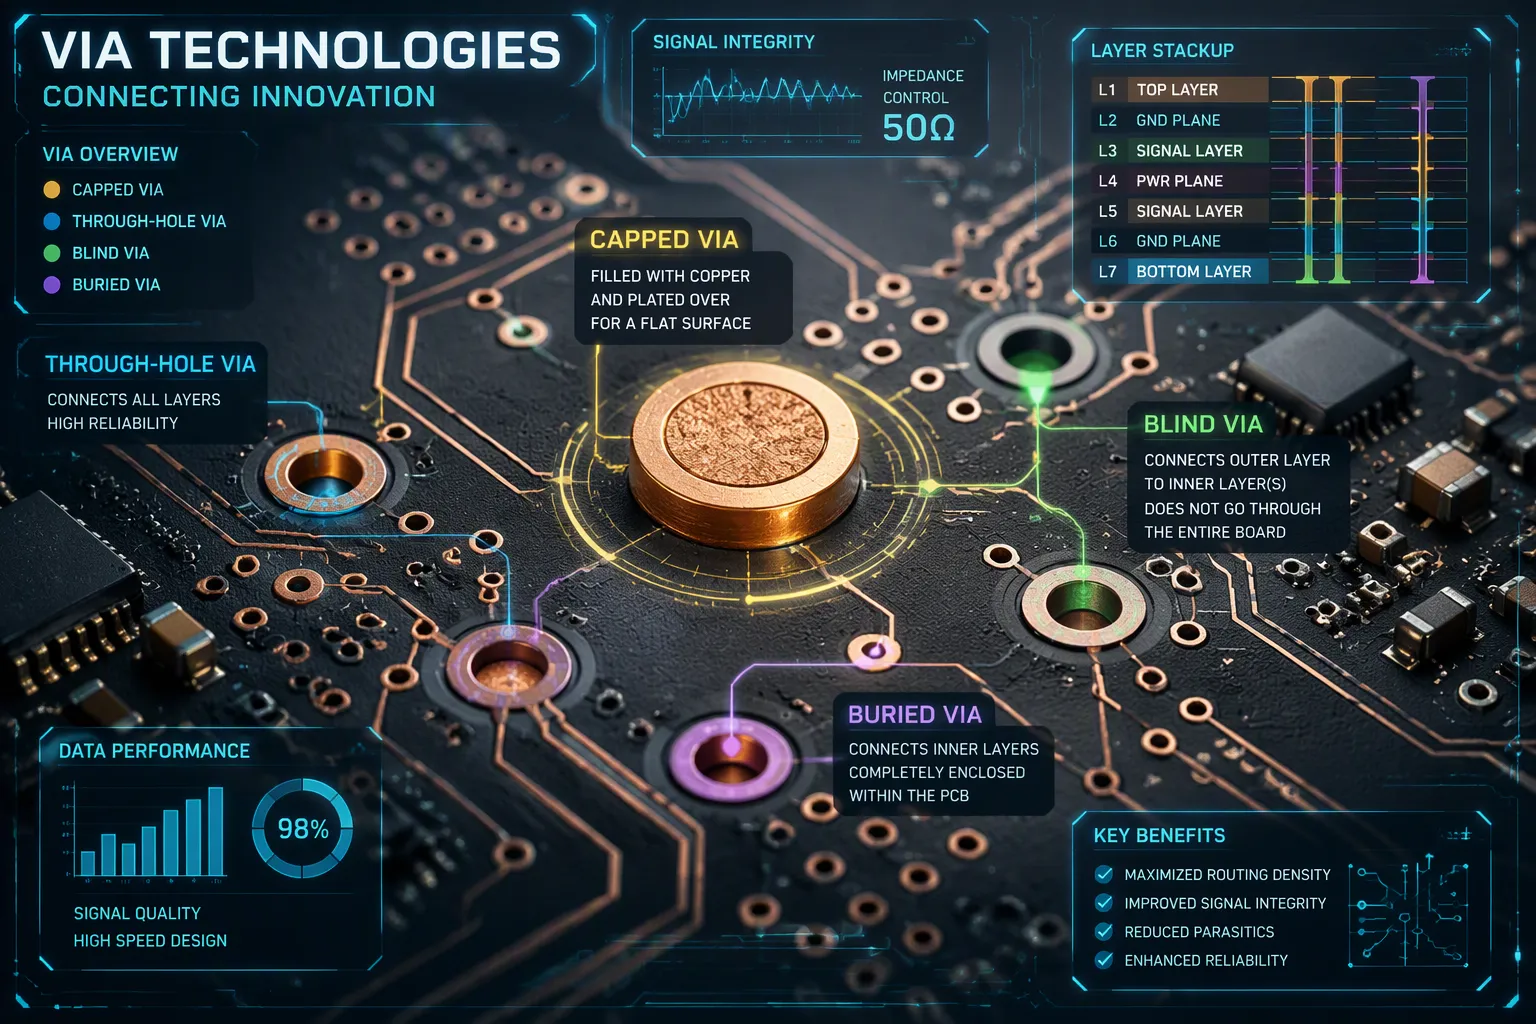
Capped vias are plated holes filled with resin and sealed with a thin copper cap. They connect layers in modern pcb designs while improving signal, thermal, and assembly performance. You face a critical choice when comparing capped vias and other via technologies across performance, reliability, cost, and manufacturability. Via selection matters greatly for HDI, high-speed, and high-density applications. Capped vias reduce weak solder joints and mechanical failures in pcbs. This article delivers a head-to-head comparison and practical guidance on when to use capped vias technology. You will learn how capped vias strengthen your next build. These pcbs benefit from careful via choices.
Key Takeaways
Capped vias fill plated holes with resin and seal them with copper, creating a flat, solderable surface.
They prevent solder wicking, reduce weak joints, and improve reliability in high-density PCB designs.
Capped vias cost 10-20% more than standard vias but save space and boost performance.
Use capped vias for via-in-pad, HDI boards, and fine-pitch BGAs at 0.8 mm pitch or below.
They offer better signal integrity and thermal management than open or tented vias.
Follow IPC-4761 Type VII standards for fill and plating to ensure quality and durability.
Avoid common failures like resin voids and cap adhesion issues with proper materials and processes.
Choose capped vias when reliability and planar surfaces are critical for your application.
What Are Capped Vias?
Definition and Core Purpose
Capped vias are plated holes that manufacturers fill with resin and then seal with a thin copper cap. This process creates a continuous metal land across the via opening. According to IPC-4761 Type VII, a capped via is defined as a via hole that has been filled and then covered with copper plating or another specified cap structure. The primary design purpose is to improve surface reliability, reduce solder-related problems, and support compact PCB layouts where ordinary open vias may create risk.
The cap prevents solder from leaking into the via during assembly. This protection matters greatly for via-in-pad designs, where a via sits directly beneath a component pad. Without a flat, sealed surface, solder wicks down into the hole and leaves a weak joint. Capped vias solve this problem by turning the via into a solderable pad. This approach also improves interconnection density in modern pcb designs.
Construction Process and Materials
The fabrication sequence involves filling and planarization before the final cap plating step. Manufacturers use epoxy resin to fill the via barrel completely. They then planarize the surface to remove excess material. A second plating cycle adds copper over the filled hole. This fill and plate the via process creates a smooth, flat surface that supports reliable component attachment.
Material selection and plating thickness follow specific standards. Epoxy resin serves as the standard fill material. Copper cap plating thickness reaches a 5 µm minimum for Class 2 products and a 12 µm minimum for Class 3 products. These requirements ensure the cap survives thermal cycling and mechanical stress. The result is a flat, sealed surface that performs like a solid pad.
Key Features and Benefits
Capped vias deliver several advantages over open or tented alternatives. They increase routing space because you can place traces directly over the via. They improve thermal management by conducting heat away from hot components. They enhance reliability through fewer weak solder joints and fewer failures from shaking or bending. The copper cap also resists contamination traps that plague exposed via openings.
The structural difference from other via types is significant. A tented via stretches solder mask over the hole like a drum skin with nothing inside. A plugged via pushes material only partway into the barrel, trapping air in the middle. Only filling fully seals the hole. A cap plate then adds a second plating cycle that closes the top. This distinction makes epoxy-filled capped vias the most robust option for demanding applications. These pcbs benefit from the superior sealing and planar surface that capped vias provide.
Overview of Other Via Technologies
Through-Hole, Blind, and Buried Vias
Through-hole vias span the entire board. They carry high current and support mechanical mounting. Unlike capped vias, they leave an open path through the stack.
Blind vias connect an outer layer to inner layers. Controlled-depth drilling recommends a production aspect ratio of 0.8:1. Buried vias sit between inner layers. Their typical aspect ratio is 4:1 to 8:1; keep it at 6:1 or lower if multiple press cycles follow. Blind, buried, and microvias differ mainly in density limits.
Via Type | Typical Aspect Ratio | Minimum Drill Size |
|---|---|---|
Through-hole (standard) | 6:1 to 8:1 | 0.2 mm |
Through-hole (advanced) | Up to 10:1 | 0.15 mm |
Through-hole (specialty) | 12:1 to 15:1 | 0.1 mm |
Blind via (mechanical) | 0.8:1 recommended | 0.15 mm standard; 0.1 mm advanced |
Buried via | 4:1 to 8:1 | Depends on sub-lamination thickness |
Via-in-Pad and Microvias
A via directly beneath a component pad saves space. Many high-density designs rely on via-in-pad with filling and capping. A copper cap seals the top. This flat pad reduces solder defects by up to 30% in high-density assemblies. It also minimizes pad damage during thermal cycling. The technique supports BGA pitches as low as 0.4 mm. Direct vertical connections shorten trace length by as much as 50%, critical for signals above 10 Gbps.
Laser drilling creates microvias through one dielectric layer. Keep the aspect ratio at 0.75:1 to 1:1. A 100 µm diameter microvia at 0.25 mm depth contributes only 0.1 nH inductance versus 1.2 nH for a standard via. Microvia diameter should not exceed 75% of pad diameter. For a 0.4 mm BGA pad, that maximum is 100 µm. When you fill and cap these openings, capped microvias offer a robust soldering surface. They suit hdi boards where space is tight. This is where capped vias outperform open microvias.
Skip and Staggered Vias
Skip vias connect non-adjacent layers by skipping intermediate layers. They can be blind, buried, or overlapped. Designers use them in BGA areas. Outer layer thickness normally stays limited to two stacks. Plan unconnected layer alignment in advance.
Staggered microvias connect layers in a spread pattern rather than stacking. Each via spans one layer. Laser drilling creates accurate connections. The design saves space and simplifies manufacturing. It also resists thermal stress. Medical monitors and factory machines often use staggered microvias. However, they require more space than stacked vias. Their offset can change impedance slightly.
Many other via types rely on open barrels that wick solder. Other via types such as skip vias need strict aspect-ratio controls. Across modern pcb designs, balance density, layer count, and assembly risk. Unlike other via technologies, capped vias seal the hole completely and create a flat pad. That seal reduces failures from shaking and bending. When you compare capped vias with through-hole or blind alternatives, reliability often outweighs extra cost. For high-density pcbs, capped vias remain the preferred solution. These pcbs demand stronger joints.
Comparing Capped Vias and Other Via Technologies
Electrical Performance
Signal Integrity and Impedance
You will see clear differences when comparing capped vias and other via technologies at high speed. A capped via creates a flat, sealed surface that keeps the pad smooth and improves signal flow. Unfilled vias leave an open barrel that traps air and disrupts signal integrity. Filled and capped vias reduce voids and air pockets that degrade high-frequency performance. Through-hole and tented vias do not consistently protect against signal loss or solder defects. For high-speed or high-frequency performance, capped vias offer a clear advantage over other via types.
Impedance control also improves with proper capping. In HDI designs, capped vias enable shorter signal paths and reduced unwanted parasitic effects. This supports faster signal transmission. The IPC 4761 Type VII standard ensures cap and fill material compatibility, which avoids air gaps and weak spots that could degrade electrical performance.
Parasitic Effects
Parasitic effects depend heavily on via structure. A filled via minimizes or eliminates the stub effect, so no distal open end reflects energy. An unfilled via acts as an open-ended transmission line and causes reflections above a few GHz. Simulations show return loss exceeding 20 dB up to higher frequencies when you fill and cap the via. Stub-resonance nulls shift or vanish. The uniform dielectric and conductor profile improves insertion loss and impedance control. Conductive filling provides a solid core and reduces loop inductance. A larger loop area around the plating barrel increases inductance, ringing, and voltage droop.
One nuance matters here. At 18 GHz, filled and hollow vias perform much the same because skin effect confines current to the barrel surface. Filling a via does not meaningfully reduce its equivalent inductance at high frequency. Capped vias mainly benefit via-in-pad assembly, thermal relief, DC current capacity, and planar solderability. They do not significantly change insertion loss or return loss at microwave frequencies when stub effects are absent.
Mechanical Reliability
Thermal Cycling and Fatigue
Capped vias reduce weak solder joints and mechanical failures during thermal cycling. The copper cap plating reaches a 5 µm minimum for Class 2 products and a 12 µm minimum for Class 3 products. These thicknesses help the cap survive repeated expansion and contraction. Unfilled and tented vias are more susceptible to fatigue because the open barrel creates stress concentration points. Capped microvias resist thermal stress better than open microvias in high-density builds.
Solder Joint Integrity
Solder joint integrity separates capped vias from other via technologies. The cap prevents solder from leaking into the via during assembly. This protection matters greatly for via-in-pad designs, where a via sits directly beneath a component pad. Without a flat, sealed surface, solder wicks down into the hole and leaves a weak joint. Capped vias solve this problem by turning the via into a solderable pad. This approach reduces solder defects by up to 30% in high-density assemblies. It also minimizes pad damage during thermal cycling.
Manufacturability and Cost
Fabrication Complexity
Standard through-hole vias stop after drilling and plating. Capped vias require filling, capping or plating over the pad, and planarization when flatness is required. Blind and buried vias add controlled-depth drilling or multiple lamination cycles. Microvias need laser drilling and precise plating. Stacked microvias demand copper filling for all but the outermost via, which is time-consuming and costly. Staggered microvias need no filling and remain more cost-effective and reliable than stacked designs.
Material and Process Costs
Cost varies widely across via technologies. The table below summarizes high-volume pricing.
Via Type | Cost per Via (High-Volume) | Key Cost Drivers |
|---|---|---|
Through-Hole Vias | < $0.01 | Simple mechanical drilling and plating |
Blind Vias | $0.05 – $0.10 | Controlled-depth drilling or laser processes |
Buried Vias | $0.05 – $0.10 | Fabrication complexity |
Microvias | $0.10 – $0.20+ | Laser drilling and precise plating |
Stacked Vias | $0.15 – $0.30 per connection | Multiple vias and alignment challenges |
Via-in-Pad (capped) | +10–20% over standard via cost | Filling and planarization processes |
Via-in-pad capping adds 10–20% over standard via cost in high volume. In low-volume or prototype runs, capping can sometimes double the PCB fabrication cost because of setup overhead. High-volume phone and computer production optimizes this to perhaps a few extra cents per via. Through vias remain the lowest-cost option and suit moderate-complexity pcbs. Capped vias cost more, but they save space and improve reliability. These pcbs benefit from smaller board size, which can offset the added process cost.
When to Use Capped Vias Technology
Ideal Applications and Design Scenarios
Choose capped vias for via-in-pad designs, hdi boards, and assemblies requiring strong solder joints and steady thermal management. When a BGA drops to 0.8 mm pitch or below, a connection in the pad becomes necessary. At 1.0 mm pitch, dog-bone fanout can serve outer rows, but inner rows often still require a pad-mounted via. Small SMT pads of 0.8 x 0.8 mm or smaller face high assembly-defect risk from capillary action. If you cannot route to a blind via, fill the hole with epoxy and cap it with copper. That cap stops solder wicking while the barrel maintains electrical and thermal connection.
Epoxy fill adds mechanical strength, maintains pad flatness, and prevents damage from trapped-air expansion during reflow. Choose an epoxy with high thermal conductivity and low electrical conductivity; the cap and barrel carry current. Specify IPC-4761 Type VII for pad-over-via construction. At 0.65 mm pitch or below, use laser-drilled microvias with copper fill. At 0.8 mm pitch and above, mechanical drilling with epoxy fill works well. Keep the via aspect ratio at 8:1 or less for reliable fill. Filled-and-capped vias create the flat pad solder paste needs; filled-only vias leave uneven surfaces and cause component tilt. A decoupling capacitor on a capped via can cut loop inductance by 3-5 times compared with dog-bone fanout. This recipe suits fine-pitch BGAs and QFNs, though large QFN thermal pads may at times use solder-mask capping.
For mainstream pcb designs with 0.8 mm pitch packages, filling adds about 15-25% to bare-board cost. That premium buys reliability. You avoid weak solder joints and improve thermal paths. When your board must survive vibration and temperature swings, these capped vias outperform unfilled or tented alternatives.
When to Choose Other Via Types
Knowing when to use other via types is equally important. On cost-sensitive, low-density pcbs, standard through-hole vias remain the first choice. They cost less than $0.01 per via in high volume, and simple mechanical drilling keeps fabrication fast. Blind and buried vias save space but add controlled-depth drilling or extra lamination cycles, at about $0.05-0.10 per via. Microvias support high-density pcb designs but cost $0.10-0.20 or more because laser drilling demands precise plating. In many boards, staggered microvias work without filling and stay more reliable than stacked designs. If your assembly includes a pad-mounted via, blind vias can sometimes replace through-hole vias in high-risk positions. In short, choose those alternatives when density, budget, or routing simplicity outweighs solder-joint risk. Choose capped vias when reliability and planar surfaces are non-negotiable.
HDI and High-Speed Considerations
For hdi and advanced designs, capped vias unlock routing space that open barrels waste. On an hdi board, every connection in the pad eliminates a dog-bone fanout and shortens the signal path. At 0.5 mm pitch or below, treat plated-over pad construction as mandatory; evaluate stacked microvias. Mechanical drilling has a practical limit near 8:1 to 10:1, with 8:1 safer. Laser microvias should stay near 1:1 or 0.8:1. On a 1.6 mm board, do not specify a mechanical drill much below 0.15-0.2 mm. A BGA pad normally measures 80-100% of ball diameter, with at least 0.1 mm annular ring per side. A 0.4 mm pad therefore allows no more than 0.2 mm via drill. Confirm dimensions with your fabricator against IPC-4761 Type VII.
These hdi pcb designs benefit most from capped vias. The flat cap supports fine-pitch placement. For high density interconnect, capped microvias create reliable soldering surfaces where open microvias would wick solder and create voids. Signal integrity improves because the filled via leaves no open stub to reflect high-frequency energy. In hdi pcbs, this reliability matters at every BGA corner. Capped vias reduce the loop inductance of decoupling paths and keep the power-delivery network quiet. For high-speed channels, the planar surface and controlled impedance make a measurable difference in jitter and eye height.
For any design that must survive harsh conditions, capped vias add a safety margin. Automotive engine control units and mission-critical aerospace electronics use this construction to resist moisture, vibration, pressure changes, and temperature extremes. The cap seals the via barrel completely, so contaminants cannot enter. This is where capped vias become the difference between field failures and long service life.
Challenges and Solutions
Challenges with Capped Vias
Capped vias issues fall into two main categories: resin voids and cap adhesion failures. Resin voids occur when trapped air or poor fill penetration leaves cavities inside the via. Narrow or high-aspect vias make complete resin filling difficult. Factory data shows roughly 0.3% of high-aspect boards above 8:1 have cap dimple defects because low plug pressure leaves a small air pocket near the top.
Cap adhesion failures stem from thin, porous, or cracked cap copper. Moisture, contamination, or oxidation weakens the bond between the cured paste and plated barrel. Inadequate hole preparation prevents reliable adhesion. CTE mismatch also plays a role. Copper paste, FR-4, and plated copper expand at different rates during thermal cycling, creating interfacial stress that cracks or delaminates the cap.
Failure Mode | Cause | Mechanism |
|---|---|---|
Resin void | Trapped air or poor fill penetration | Air cavities remain inside the via and reduce mechanical support |
Cap adhesion failure | Thin, porous, or cracked cap copper | Weak cap surface exposes the fill and reduces solderability |
Cap cracking | CTE mismatch | Repeated soldering creates interfacial stress |
Resin outgassing | Reflow above 170°C | Trapped gas releases and causes solder voiding |
Challenges with Other Via Types
Unfilled vias wick solder during reflow. Molten solder drawn by surface tension along plated walls depletes joint volume on adjacent pads. This causes head-in-pillow defects, insufficient standoff, and reduced mechanical strength. Larger vias above 0.3 mm pose greater risk because capillary forces increase.
Solder wicking occurs when molten solder encounters an open via during reflow, drawn in by surface tension and wetting along the plated walls. This depletes the solder joint volume on adjacent pads, often resulting in head-in-pillow defects or insufficient standoff.
Tented vias face mechanical stress. The solder mask tent relies on adhesion and tensile strength. Excessive via-to-mask clearance or mask overexposure weakens the tent. Tent softening above 200°C during reflow causes tears and delamination. Blind, buried, and microvias add cost and complexity. Stacked microvias demand copper filling for all but the outermost via, which is time-consuming and costly.
Mitigation Strategies
Follow IPC guidelines to prevent these failures. IPC-6012 performance classes specify fill material selection, aligning copper versus epoxy with CTE and conductivity needs. IPC-2226 aspect-ratio rules control achievable void-free fill. IPC-4761 Type VII governs copper-filled stacked microvias. Avoid placing laser microvias directly over epoxy-filled mechanical vias because the soft epoxy foundation can cause delamination.
Use proper materials and optimize processes. Clean via geometry and thorough desmear remove resin residue for uniform metallization. Pulse-reverse plating with controlled current density promotes bottom-up fill and suppresses voids. Planarization to 5-10 µm dimple reduces residual-dimple solder voiding. Perform reliability testing with IPC-TM-650 methods. IST, thermal shock, and vibration testing detect barrel cracking and interfacial separation before qualification. These steps keep your capped vias reliable in hdi and high-speed pcb designs.
IPC 4761 Type VII and Standards
Overview of IPC 4761 Type VII
IPC 4761 Type VII defines the requirements for conductive fill with a metal cap. This standard covers filling and plating requirements for capped vias in high-reliability applications. You will find that Type VII demands conductive fill, such as electrolytic copper or conductive epoxy, capped with copper plating. This construction is required for high-reliability applications per IPC-6012 Class 3/A.
The standard specifies that cap plating must withstand five solder floats at 288°C per IPC-TM-650 2.4.13. Surface dimple after cap plating must not exceed 15 μm, with 10 μm typically achievable. These requirements ensure your capped vias survive assembly and field conditions. When you specify ipc 4761 type vii standards, you establish clear acceptance criteria for your fabricator.
Other Relevant Standards
IPC-6012 and IPC-2221 provide supporting requirements for via plating and annular ring. IPC-6012 serves as the primary specification for annular ring acceptance criteria on rigid pcbs. IPC-2221 offers land pattern and fabrication allowance guidance. IPC-A-600 provides visual inspection criteria.
Requirement | IPC-2221 | IPC-6012 Class 3 |
|---|---|---|
Annular ring applicability | Applied universally for Class 1–3 products | Breakout allowed for all but Class 3 |
Breakout allowance | Not allowed (IPC-2221A) | Not allowed for Class 3 |
Minimum hole wall plating | — | 0.8 mil (Class 1 & 2); 1 mil (Class 3) |
Class 3 leftover annular ring | — | Required (some leftover ring must remain) |
Class 3 external layer minimum annular ring measures 0.001969" from the inner diameter of the finished plated hole to the shortest edge of the plated land. Class 3 internal layer minimum annular ring measures 0.000975" from the drill diameter to the shortest distance to the edge of the land. Class 2 allows 90° breakout with a teardrop at the land-conductor junction. Review IPC-2221 Section 9.1.1 and Table 9-1 to determine required annular ring based on design complexity.
Compliance and Testing
You must verify compliance through multiple test methods. Microsection evaluation requires minimum 32 cross-sections per IPC-6012. This assesses void area, dimple, barrel thickness, and fill completeness. Thermal shock testing uses six solder floats at 288°C for 10 seconds per IPC-TM-650 2.4.13. A passing result shows no barrel cracking, delamination, or fill separation.
Acceptance Parameter | IPC-6012 Class 3 | Class 3/A |
|---|---|---|
Void area (per cross-section) | < 25% | < 10% |
Surface dimple | ≤ 15 μm | ≤ 10 μm |
Barrel plating thickness | ≥ 20 μm copper | N/A |
Thermal cycling qualification | N/A | 200 cycles per IST |
IST requires 500+ cycles to failure, with minimum 200 cycles for Class 3/A. CAF testing per IPC-TM-650 2.6.25 checks for conductive filament growth at 85°C/85% RH, 100 V DC bias, 500 hours. Thermal cycling from −55°C to +125°C for 100 cycles minimum per IPC-TM-650 2.6.7.2 passes when resistance change stays below 10%. These tests confirm your capped vias meet reliability targets.
You now see the trade-offs clearly when comparing capped vias and other via technologies. Capped vias deliver lower signal loss, better heat transfer, and more thermal cycles than unfilled options, at a 10–20% cost premium. Through-hole vias stay cheapest and simplest, while blind, buried, and microvias save space with added process steps.
For HDI and via-in-pad designs, capped vias win on signal integrity, thermal management, and assembly reliability. Evaluate your density, budget, and reliability targets, then specify IPC 4761 Type VII for your pcbs.
FAQ
What exactly is a capped via?
A capped via is a plated hole filled with resin and sealed with a thin copper cap. The cap creates a flat, solderable surface. This construction prevents solder from wicking into the barrel during assembly. IPC-4761 Type VII defines the fill and plating requirements for this via type.
How much more do capped vias cost?
Via-in-pad capping adds 10–20% over standard via cost in high volume. Prototype runs can sometimes double fabrication cost because of setup overhead. Through-hole vias remain the cheapest option at under $0.01 per via. The premium buys reliability and smaller board size.
When should I choose capped vias over through-hole vias?
Choose capped vias for via-in-pad designs, HDI boards, and fine-pitch BGAs at 0.8 mm pitch or below. Through-hole vias suit cost-sensitive, low-density boards. Capped vias reduce solder defects by up to 30% in high-density assemblies. Reliability often outweighs the extra process cost.
Do capped vias improve signal integrity at high frequencies?
Capped vias eliminate the open stub that causes reflections above a few GHz. Filling removes air pockets and supports controlled impedance. At 18 GHz, filled and hollow vias perform much the same because skin effect confines current to the barrel surface. The main benefit remains assembly reliability and thermal relief.
What plating thickness does IPC-4761 Type VII require?
IPC-4761 Type VII requires a 5 µm minimum copper cap for Class 2 products and a 12 µm minimum for Class 3 products. The cap must withstand five solder floats at 288°C per IPC-TM-650 2.4.13. Surface dimple after plating must not exceed 15 μm.
Can I place a capped via directly under a BGA pad?
Yes. Via-in-pad with filling and capping supports BGA pitches as low as 0.4 mm. The flat cap stops solder wicking and reduces pad damage during thermal cycling. Direct vertical connections shorten trace length by as much as 50%, which matters for signals above 10 Gbps.
What causes cap adhesion failures?
Thin, porous, or cracked cap copper weakens the bond between the cured paste and plated barrel. Moisture, contamination, or oxidation also degrades adhesion. CTE mismatch between copper paste, FR-4, and plated copper creates interfacial stress during thermal cycling. Proper hole preparation and desmear prevent these failures.
How do I verify capped via reliability?
Microsection evaluation requires a minimum of 32 cross-sections per IPC-6012. Thermal shock testing uses six solder floats at 288°C. IST requires 500+ cycles to failure, with 200 cycles minimum for Class 3/A. CAF testing checks for conductive filament growth at 85°C/85% RH.
