How to Inspect and Control Microvia Quality in HDI PCBs
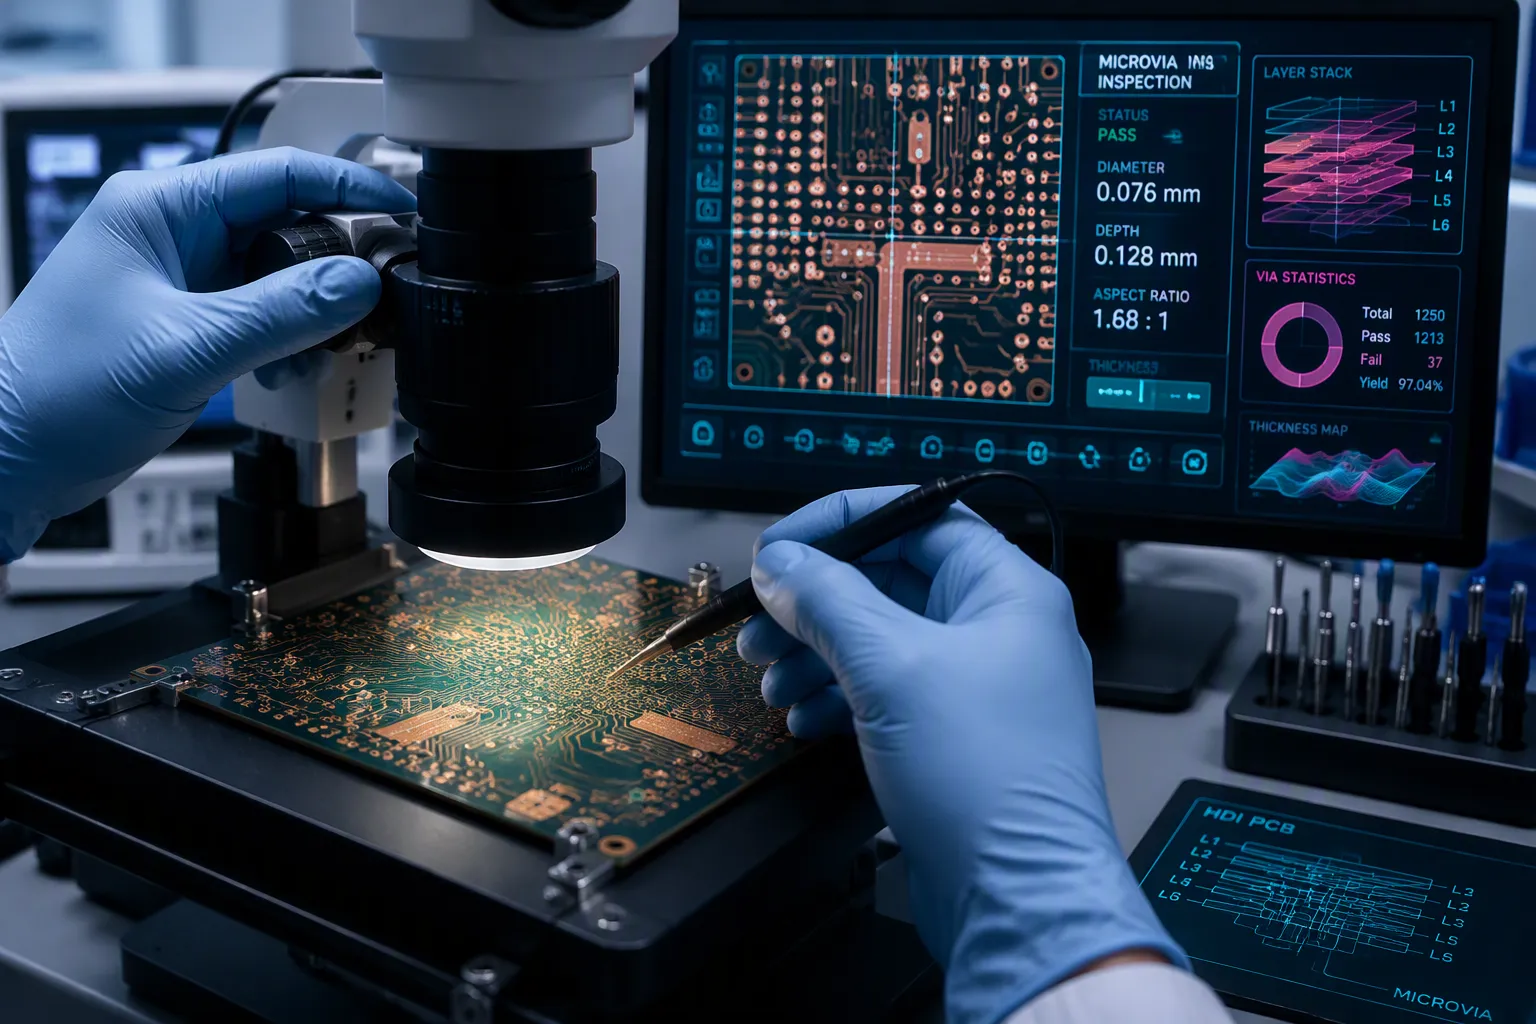
Microvia integrity decides how reliable your HDI design will be. High density interconnect technology uses microvias to make shorter trace routes and smaller diameters. This gives better performance than regular boards. But defects like voids or cracks can cause open circuits or failures. You cannot afford these flaws in critical applications. One bad via can ruin a whole board.
You inspect microvias by looking at them, cross-sectioning, X-ray, automated optical inspection, and electrical testing. Each method finds different kinds of defects. Visual checks find surface problems, while X-ray shows hidden voids. HDI PCB Quality Control needs careful material selection, precise drilling parameters, thorough desmear, uniform plating, proper filling, and smart design choices. You compare staggered versus stacked vias for reliability.
Key Takeaways
Use visual checks, X-ray, cross-sectioning, and electrical tests to find different microvia defects.
Control material choice, drilling, desmear, plating, and filling for good microvia quality.
Pick staggered vias instead of stacked ones for better reliability under heat stress.
Follow IPC rules, such as IPC-6012, for plating thickness and void limits.
Check microvias at every production step to find problems early and keep them reliable.
HDI Micro-via Inspection Techniques
You need a step-by-step inspection plan to find micro-via defects at each stage. Each method shows different problems. No single technique catches everything.
Visual and Optical Inspection
You begin with visual checks using a magnifier. Look for surface defects, color changes, and pad shape issues. A good micro-via has a clean, centered pad with even copper. Plating defects often leave visible signs. The table below shows what you can find.
Defect Type | Visual Indicator | Condition / Cause |
|---|---|---|
Voids | Microvia mouth closes too early with big empty spaces inside | Low NBT concentration (10–20 ppm); little copper at via bottom while mouth deposits quickly |
Non-uniform copper thickness | Clear uneven surface (Rq 113.0 nm, Ra 131.9 nm) | Only PEG and SPS present; NBT addition slowly smooths surface (40 ppm NBT: Rq 27.8 nm, Ra 37.2 nm) |
Nodulation | Separate bumps on the deposit surface | Higher NBT concentration; uneven NBT coverage or local cathodic reduction of extra NBT into solid bits |
These signs help you mark suspect boards before they move on. Automated optical inspection (AOI) adds to visual checks for ultra HDI boards. You set up AOI with correct pad shape and spacing rules. Design-for-inspection practices matter here. Tight spacing between micro-via pads can trick the camera. Give the system clear contrast and steady fiducials.
Cross-Sectioning and X-Ray
Cross-sectioning gives you the real truth about microvia quality. You mount a sample, grind it down, and polish it. Then you look at the via wall under a microscope. Measure wall thickness and fill quality. A good micro-via has even copper along the barrel and full fill with no gaps. This step proves what visual checks suggest.
X-ray inspection finds hidden problems. You use it for buried or blind microvias. Voids, cracks, and misregistration show up clearly. X-ray works well for stacked via structures where cross-sectioning is hard. You can check many boards without destroying them.
Electrical testing closes the loop on electrical integrity. Continuity tests confirm the micro-via conducts. Resistance measurements catch weak connections. Reliability screening with thermal cycling stresses the board. You watch for resistance shifts that signal cracks. This step matters for a pcb that must survive harsh use.
Combine these methods for full coverage. Visual and AOI catch surface issues fast. Cross-sectioning and X-ray verify internal structure. Electrical testing proves function. Together they form a complete inspection framework for any HDI design.
HDI PCB Quality Control Measures
You control microvia quality at every step of manufacturing. Material choice, drilling precision, desmear chemistry, plating uniformity, and micro-via filling all matter. Each step builds on the one before it. This section shows you how to keep each step under control.
Material and Drilling Control
Your material selection starts the hdi pcb quality control chain. Pick laser-friendly dielectrics for cleaner via barrels. Standard laminates can burn or leave rough hole walls. Match copper foil thickness to what your design needs. Thin foil makes drilling easier. Thick foil carries more current. Your stackup decides the right balance.
Drilling settings directly change microvia quality. Set laser power and pulse width for your material. Too much power burns the dielectric. Too little power leaves incomplete vias. Control via size and volume with care. A typical micro-via in an HDI board needs a certain depth-to-diameter ratio. Follow your material supplier's guidelines for the best results.
Desmear removes drilling residue from the via walls. You have two main routes: plasma or chemical permanganate. Each one removes residue in a different way.
Decision point | Plasma route | Chemical (permanganate) route |
|---|---|---|
Removal mechanism | Gas-phase reaction with organic residue | Wet chemical oxidation and conditioning |
Material fit | Selected high-performance resins and small features when qualified | Many conventional multilayer constructions |
Access | Chamber loading and gas transport into holes | Solution exchange and wetting |
Process control | Power, pressure, gas, time, and load geometry | Concentration, temperature, dwell, agitation, and bath loading |
Verification | Hole-wall evidence on representative samples | Hole-wall evidence on representative samples |
Both routes need control and evidence for each construction. Plasma desmear uses a controlled low-pressure plasma to remove organic drilling smear. It prepares the hole walls before electroless copper and plating. It changes the polymer surface to improve wetting and adhesion. One manufacturer saw a huge drop after installing plasma desmear:
After installing a plasma desmear unit in production, the manufacturer observed a dramatic reduction in incidences of pink ring and wedge voiding, and consequently in desmear-related scrap. This indicates that plasma desmear improved via wall activation and plating adhesion compared to the prior permanganate-based process.
For chemical permanganate, follow three steps. First, apply an alkaline solvent swell to help remove epoxy-resin smear. Second, use a permanganate bath in alkaline solution heated to 160°F or higher to remove drill smear. Third, use an acidic neutralizer to remove all traces of alkalinity and oxidizer.
Plating completes the via connection. Control chemistry for even deposition. Keep plating thickness the same across complex HDI structures. Thin plating at the via base causes cracks later. Good hdi pcb quality control ties these steps into a reliable process.
HDI PCB Micro-via Filling Control
Micro-via filling closes the via with copper. Poor filling leaves voids that trap chemicals or create stress points. You cannot afford gaps in critical HDI boards. The importance of micro-via filling becomes clear when you see a failed board from incomplete fill.
The micro-via filling process needs careful parameter control for quality copper deposition. You need the right plating chemistry, current density, and agitation. A good fill has no voids and a flat surface. This allows reliable stacking of more layers on top.
A step-by-step micro-via filling process starts with hole preparation. Clean the via walls after desmear. Apply a seed layer for even copper coverage. Set plating parameters for bottom-up fill. Monitor bath chemistry for consistency. Inspect fill quality with cross-sectioning. Verify via integrity after filling with electrical tests.
Inspect fill quality after each plating run. Look for voids at the via base or center. Check for surface dimples that signal incomplete fill. Measure filling height compared to via depth. A fully filled micro-via meets your design requirement.
Design choices affect filling success. Staggered vias allow tighter spacing between microvias. Keep at least 2 mil spacing between staggered microvias. Stacked vias need careful filling control. Control spacing between laser vias and through-hole vias to avoid resin flow issues. These pcb design decisions directly impact hdi pcb micro-via filling reliability.
Your pcb design rules should match your filling capability. Tight spacing makes filling harder. Deep vias need longer fill cycles. Work with your manufacturer early to set realistic design rules. Good hdi pcb micro-via filling outcomes depend on both process and design.
Every step in this control chain matters. Material choice, drilling precision, desmear chemistry, plating uniformity, and micro-via filling all determine your final quality. You cannot skip one step and expect good results. HDI pcb quality control means managing every variable together.
Micro-via Defect Troubleshooting
Voids, Cracks, and Incomplete Fill
You will find four common defects in micro-via work: voids, cracks, incomplete fill, and barrel separation. Each one comes from a different root cause. Voids often happen when the filler material lacks additives. Copper then builds up on the walls and surface instead of filling the via body. Conformal plating makes this worse. Incomplete desmear and resin residue from laser drilling also trap gas and block proper filling. Cracks and barrel separation usually happen after thermal stress when the plating is thin or uneven.
Your fix starts with the micro-via filling process. Additives help copper deposit evenly along the via body. They stop voids, dimples, and bumps. Reverse pulse plating adjusts additive concentrations for uniform bottom-up growth. This stops copper from building up on the walls and surface. Check your desmear chemistry and drilling parameters next. A poor micro-via filling process will hurt the impact on electrical performance and weaken microvia reliability over time.
Staggered vs. Stacked Via Design
Your pcb design choices decide how much stress each microvia carries. Stacked vias place every layer right on the one below. This saves space but puts all thermal stress in one column. Staggered vias offset each layer. They spread the stress and improve microvia reliability. Keep at least 2 mil spacing between staggered microvias. Also control spacing between laser vias and through-hole vias.
Empirical data and highly accelerated thermal shock (HATS) testing consistently demonstrate that staggered microvia configurations survive significantly more thermal cycles before failure compared to their stacked counterparts.
Use this data when you set pcb design rules. Stacked vias still work for low-stress boards. For demanding hdi products, staggered layouts give you better reliability. Match your via style to the thermal load your pcb will face.
Reliability in HDI PCB and Standards
Key IPC Standards
You need accepted benchmarks to judge microvia quality. The IPC-6010 series gives you that framework. IPC-6016 is the HDI-specific standard. It covers build-up layers rather than the core. Its criteria break down by slash sheet categories like chip carrier, hand held, high performance, harsh environment, and portable. IPC-6012 covers rigid boards and sets clear limits for microvia reliability. It requires a minimum 15 µm plating thickness for microvia barrels. It also caps void volume in filled microvias at 5%. A board must survive 1,000 thermal cycles from -40°C to 125°C without cracking or delamination.
Standard | Covered criteria for HDI microvia acceptance |
|---|---|
IPC-2226 | Design rules: finished hole diameter ≤150 µm, aspect ratio ≤1:1, minimum annular ring 25 µm, minimum center-to-center clearance 50 µm, and microvia-in-pad filling with minimum pad diameter of 3× the via diameter |
IPC-6012 | Minimum 15 µm plating thickness for microvia barrels; maximum 5% void volume in filled microvias; 1,000 thermal cycles from -40°C to 125°C without cracking or delamination |
IPC-6013 | Flexible boards: 100,000 flex cycles at 180° bend without electrical failure; minimum peel strength of 0.5 N/mm between microvia plating and substrate |
IPC-TM-650 | Test methods: cross-sectional analysis for copper thickness, void presence, and plating uniformity; thermal cycling; mechanical shock testing |
IPC-6012F is the current revision. It adds performance-based testing for microvia structures. Addendums cover automotive, space and military, and medical applications. Use these standards as your acceptance baseline.
Industry Best Practices
Strong hdi pcb quality control depends on routine checks at every stage. Inspect microvia quality after drilling, after filling, and after plating. Cross-section representative samples from each lot. Track plating thickness and void volume against IPC-6012 limits. Keep desmear chemistry within its window. Monitor filling parameters for bottom-up growth. These habits catch defects before they reach assembly.
Design for reliability from the start. Choose staggered vias over stacked ones for high-stress boards. Keep at least 2 mil spacing between staggered microvias. Control spacing between laser vias and through-hole vias. Match your via style to the thermal load your pcb will face. A high density interconnect board in a harsh environment needs more margin than a consumer device.
Your control plan should tie inspection frequency to process stability. Stable processes need less frequent sampling. New or changed processes need more. Document every result. Feed findings back into design rules and plating parameters. This loop keeps microvia reliability high across production runs. Strong quality checks in HDI manufacturing keep boards free from mistakes for demanding applications. Reliability in hdi pcb comes from consistent process control, not from a single inspection step.
You now have a complete set of tools for checking your boards. Visual checks, cross-sectioning, X-ray, AOI, and electrical tests each find different micro-via problems. Control steps cover materials, drilling, desmear, plating, micro-via filling, and design. Filling quality needs extra care. Bad filling leaves empty spaces. Good filling keeps microvia reliability strong. Filling control begins with clean via walls. Filling settings must fit your design. Filling inspection checks every via. Filling flaws weaken microvia reliability. Filling success comes from steady process habits. Filling and design must work as a team. No single step promises quality. You need a whole approach. Mix inspection, process control, and standards. Use these practices early in design and manufacturing. This cuts defects and boosts hdi pcb results.
FAQ
What plating thickness does IPC-6012 require for microvia barrels?
IPC-6012 requires at least 15 µm of plating on microvia barrels. Thin plating at the bottom of the via can crack when it gets hot. You should check this number using cross-sectioning on sample boards from each lot. Compare your results to the standard and use them to adjust your plating settings.
How much void volume is acceptable in a filled microvia?
IPC-6012 allows no more than 5% void volume in filled microvias. Voids trap chemicals and create weak spots that hurt reliability. After each plating run, check fill quality with cross-sectioning. Look for gaps at the bottom or middle of the via, and check for surface dimples that mean the fill is not complete.
Why do staggered microvias last longer than stacked ones?
Stacked vias put all the heat stress from every layer into one column. Staggered vias shift each layer over and spread that stress out. HATS testing shows staggered setups survive many more heat cycles before they fail. Keep at least 2 mil of space between staggered microvias, and control the space between laser vias and through-hole vias.
What design rules does IPC-2226 give for microvias?
IPC-2226 limits the finished hole diameter to 150 µm or less and the aspect ratio to 1:1. It also requires a minimum annular ring of 25 µm and at least 50 µm of center-to-center clearance. For microvia-in-pad, the pad diameter must be at least 3× the via diameter.
Which defects show up most often in microvia work?
Voids, cracks, incomplete fill, and barrel separation are the four common defects. Voids come from missing additives or trapped gas. Cracks and barrel separation happen after heat stress when plating is thin or uneven. Fixes include additive control, reverse pulse plating, and tighter desmear chemistry.
See Also
Mastering Quality Control Methods For Printed Circuit Board Production Processes
Explore Modern High Density Interconnect Prototype Methods Right Now
Advantages Of Laser Direct Imaging Exposure Machines For HDI Circuit Production
How Laser Direct Imaging Application Affects Overall Quality Of PCB Products
Seven Essential Quality Control Steps For High Current Heavy Copper PCB Assembly In Cars
